Matched Planer-Knife Set Control in a Shared Toolroom
Learn how shared toolrooms preserve matched planer-knife sets with a straight knife grinder using traceable IDs, checks, and handover controls.

Matched Planer-Knife Set Control with a Straight Knife Grinder
In a shared toolroom, a straight knife grinder is only part of the process. Planer knives may move between production lines, shifts, and storage racks, so a matched set can be separated before it returns to service. A simple identity-and-handover workflow helps maintenance teams preserve set membership, compare grinding results, and avoid installing knives with inconsistent histories.
Why matched sets need their own identity
Assign one permanent set ID to every group intended to run together, then mark each knife with its position within that set: for example, Set A / 1, Set A / 2, and Set A / 3. Record the knife type, current usable width, previous grinding date, and the machine or production line it serves. This is more useful than a general rack label because the record stays with the knives through inspection, grinding, storage, and issue.
Separate records are especially important when a toolroom handles planer knives alongside veneer knives, paper knives, or chipper knives. Similar-looking blades can have different clamping needs, wheel requirements, and acceptance criteria. A set card should identify the required fixture, coolant practice, and any handling notes without assuming that one setup suits every knife.
Straight knife grinder checks before sets are released
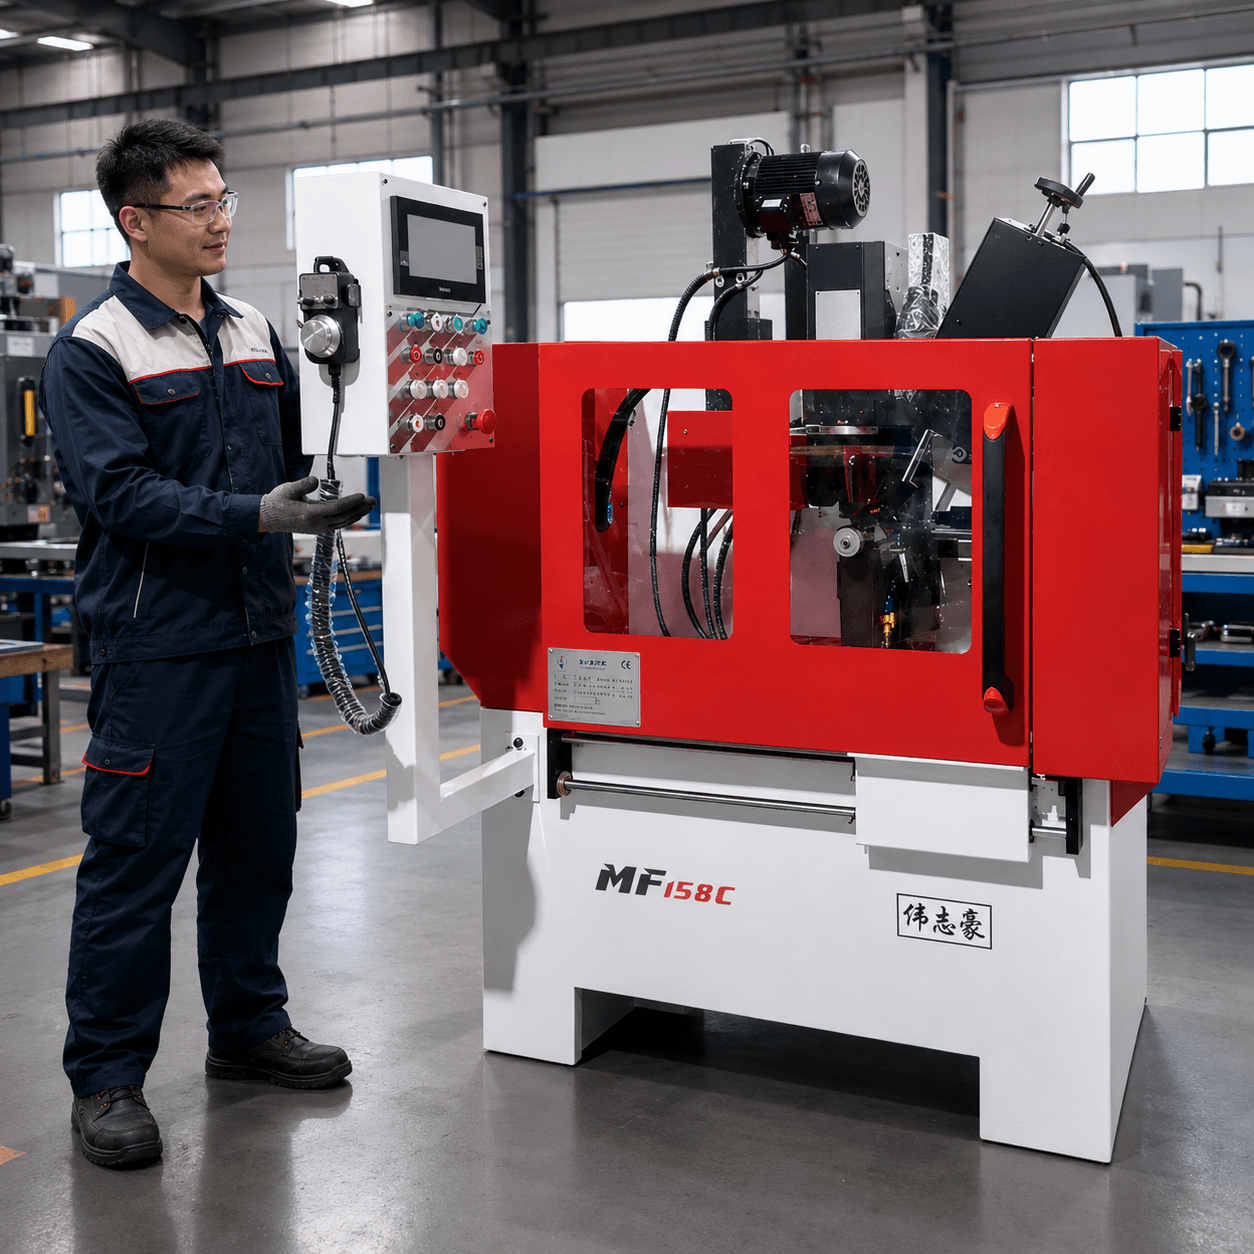
Before loading a set, the operator should compare each knife with the set card and confirm that all members are present. Check the quoted knife width range against the actual workpieces, select the correct magnetic chuck or clamp chuck, and verify that the support and clamping arrangement is appropriate for the knife. A planer blade sharpener process should keep knives in their identified order rather than mixing them into a general batch.
After grinding, inspect the set as a group. Record the measured result against the buyer’s required straightness tolerance, note any knives removed from service, and keep the final identification visible during transport to storage. If a replacement knife is introduced, give it a clear link to the set record and flag it for the production team. These controls make discrepancies visible before installation rather than after a quality complaint.
What buyers should request during evaluation
When assessing a planer knife grinder, ask the supplier to clarify capacity, supported knife width range, available tooling and fixtures, chuck type, coolant arrangement, and the inspection method used for acceptance testing. Confirm which grinding wheels and other consumables are included or recommended, plus what first-run training covers. Review the relevant straight knife grinder category and compare it with the wider blade grinding machine range where the toolroom processes multiple industrial knife types.
For shipment inspection, buyers can request identification of the supplied fixtures and documented test conditions that reflect their inquiry data. Weizhihao manufactures relevant sharpening and grinding equipment and can use a complete application description to support a clearer technical discussion.
Prepare a quote-ready set-control brief
Send the number of knives per set, knife dimensions, material, application, required straightness tolerance, preferred chuck type, coolant needs, power details, and expected grinding volume. Include photographs of unusual knife shapes or existing fixtures. Browse the Weizhihao product range, then use the quote request contact page to discuss a suitable configuration, training expectations, and acceptance checks.
FAQ: Should every knife in a matched set have a separate mark?
Yes. A shared set ID plus an individual position number helps operators confirm that every member is returned and retained in its intended order.
FAQ: Is a magnetic chuck always the right choice for planer knives?
No. Buyers should confirm knife material, dimensions, workholding requirements, and whether a magnetic chuck or clamp chuck best suits the application.
FAQ: What should a set record include after grinding?
Include the set ID, date, operator, grinding result, straightness-tolerance check, usable width, wheel or fixture notes, and any replacement action.
FAQ: What information helps a supplier prepare a useful inquiry response?
Provide knife drawings or photographs, length and width range, quantity per set, application, desired tolerance, coolant preference, electrical requirements, and training needs.